


News Center
—— NEWS CENTER ——
Xi'an Shenghongchuang Instrument Co., Ltd.
Contact: Mr. Zhang
Mobile: 15529283736
Email: shc-sensor@qq.com
Address: Fortune Building, Sanqiao Street, Xixian New Area, Xi'an, Shaanxi Province
Which industries are suitable for level sensors with good linearity? Application scenarios, signal selection, and key usage considerations
From chemical storage tanks to smart manufacturing, stable and accurate level measurement is an important foundation for automated control. A level sensor with good linearity generally refers to a measuring device whose output signal remains highly consistent with actual level changes. For example, for every 1% change in level, the output current, voltage, or digital communication data changes steadily in the corresponding proportion.
For industrial sites requiring continuous monitoring, interlock protection, remote display, or automatic replenishment, linearity directly affects control accuracy. If signal drift is significant or repeatability is insufficient, PLCs, instruments, or host computers may receive incorrect data even when the liquid level in the vessel changes only slightly, thereby affecting pump start-stop operation, valve opening, and production cycle times.
Leveraging the production and technical capabilities of Shaanxi Qinkong Sensor Technology Co., Ltd., Xi'an Shenghongchuang Instrumentation Co., Ltd. can provide suitable solutions for measurement and control requirements involving pressure-type, submersible, hydrostatic, flange-type sensors, and supporting intelligent digital display instruments. Actual selection should not focus solely on “good linearity”; the medium, installation method, temperature and pressure conditions, signal interface, and maintenance cycle must also be considered comprehensively.
The following addresses common questions regarding level sensor use from the perspectives of industry applications, operating condition assessment, communication methods, and procurement evaluation, helping project personnel establish a clearer selection approach.
I. Which Industries Are Suitable for Level Sensors with Good Linearity
Level sensors with good linearity are widely used in industries requiring continuous level data, rather than being limited to simple high- and low-level alarms. Chemical processing, energy, water treatment, food processing, machinery support, logistics and warehousing, metallurgy and building materials, and environmental monitoring all involve liquid storage, batching, metering, or process control requirements.
In chemical storage tank applications, level data is often linked to feed volume, reaction progress, and safety margins. For media such as acid and alkali solutions, organic solvents, and cleaning fluids, it is necessary to first confirm whether wetted materials are corrosion-resistant, and then consider measuring range and output accuracy. Common projects reserve a 10% to 20% measuring range margin to avoid mechanical shock or overpressure risks caused by long-term full-scale operation.
In smart manufacturing and automated production lines, level sensors are commonly installed in lubricating oil tanks, coolant tanks, cleaning fluid tanks, batching tanks, and process water tanks. The control system uses continuous signals to perform liquid replenishment, alarms, shutdown protection, and data traceability. If equipment operates at a fast cycle rate, repeatability, response time, and electromagnetic compatibility should be key evaluation factors.
In wastewater treatment, water supply, and environmental monitoring systems, the level measurement range may vary from several hundred millimeters to dozens of meters. Such operating conditions typically place greater emphasis on long-term stability, waterproof construction, and the reliability of on-site wiring. For locations such as outdoor pools, deep wells, and underground pumping stations, cable protection, lightning surge protection, and moisture condensation should also be considered.
Typical Industries and Key Considerations
II. How to Assess Sealing and Materials Under Complex Operating Conditions
Will a sealed level sensor leak when used in coal mines?
Whether a sealed level sensor can be used in a coal mine cannot be determined simply by saying that it “will leak” or “will not leak.” Qualified products should provide corresponding sealing performance under rated pressure, specified temperature, and proper installation conditions. However, mine environments are often accompanied by humidity, dust, vibration, corrosive water quality, and cable pulling, placing higher requirements on the housing, cable outlet, wiring chamber, and installation interface.
Coal mine projects should first confirm whether the equipment complies with the explosion-proof, protection, and site safety specifications required by the project. For underground applications, in addition to the sensor itself, the power supply method, junction box, explosion-proof accessories, shield grounding, and maintenance procedures are equally important. Directly replacing dedicated mining configurations with ordinary industrial products can easily create safety and acceptance risks.
Common causes of sealing failure include installation threads not being handled in accordance with specifications, incompatibility between sealing rings and the medium, continuous cable pulling, an undersized measuring range, and pressure shocks exceeding the rated range. After installation, verification can be conducted through pressure-holding checks, zero-point observation, and periodic inspections, rather than neglecting subsequent maintenance simply because the initial readings are normal.
For sewage pits, drainage chambers, or mine water tanks, if the medium contains sediment, particulates, or suspended matter, it is recommended to assess the probe installation position and avoid placing it directly in sedimentation areas. Submersible level products should use fixing devices to control the probe position and reduce swinging, collision, and cable wear.
Can PTFE level sensors be installed in strong acids?
Polytetrafluoroethylene materials offer good corrosion resistance and are therefore commonly used for wetted parts in strong acids, strong alkalis, and certain corrosive media. However, the use of PTFE does not mean that the entire sensor is suitable for all strong-acid operating conditions. The actual materials of the diaphragm, seals, pressure transmission structure, flange lining, and cable sheath must also be verified.
The concentration, temperature, and impurity content of strong acid media can significantly alter the degree of corrosion. For example, material compatibility is not exactly the same under ambient and high-temperature conditions. Crystallization, precipitation, or volatile gases in the medium may also affect the measuring diaphragm and installation chamber. When selecting a model, the medium name, concentration range, maximum temperature, and vessel pressure should be provided in full.
For corrosive liquids that are prone to crystallization or adhesion, flange-type, diaphragm-type, or easy-to-flush installation structures should be considered to reduce the risk of pressure ports becoming blocked. Pursuing a lower purchase price alone while ignoring wetted materials often results in shortened sensor life, measurement distortion, or even leakage.
Before procurement, the manufacturer should be required to specify the materials of wetted parts, rated working pressure, temperature resistance range, and application limitations. For high-risk operating conditions, small-batch trial installation can be conducted first, and zero point, full scale, and signal fluctuation should be recorded during initial operation to provide a basis for subsequent batch configuration.
III. How to Choose Between Analog Signals and Digital Communication
Can an RS232 level sensor be connected to a PLC?
An RS232 level sensor can be connected to a PLC, provided that the PLC has a corresponding serial communication interface or is matched through a communication module or serial converter. RS232 is generally suitable for point-to-point, short-distance communication and is more commonly used in engineering for equipment commissioning, instrument parameter setting, or short-distance data reading.
The communication protocol must be confirmed before connection; interface appearance alone is not sufficient. Both sides should maintain consistency in parameters such as baud rate, data bits, stop bits, parity method, station number, and register address. Even if both use RS232 interfaces, the PLC still cannot correctly identify level data if the protocol formats differ.
When multiple sensors need to be networked on site, wiring distances are long, or interference is strong, RS485 is generally more suitable for industrial applications. It supports multi-node communication, and its differential transmission method offers better common-mode interference resistance. During engineering implementation, shielded twisted-pair cable should be used properly, with terminal resistors and grounding methods set appropriately.
If a project already has a PLC, touch screen, DCS, or IoT gateway, the existing interface list should be compiled before determining the sensor output. This avoids adding conversion modules, modifying programs, or rewiring after equipment arrives due to interface incompatibility.
Which is better: a HART protocol level sensor or 485?
There is no absolute advantage or disadvantage between HART and RS485; the key lies in the control system architecture. HART is generally based on a 4-20mA analog current loop and enables digital communication while retaining analog primary variable output. It is suitable for process industry projects with existing analog systems that require remote diagnostics and parameter management.
RS485 is common in communication applications such as Modbus RTU and is suitable for centralized collection from multiple devices, digital display instrument networking, PLC control cabinets, and automated production lines. For scenarios requiring multiple level, pressure, and temperature instruments to be connected on the same communication bus, 485 wiring and data management are generally more convenient.
A 1-5V level sensor can maintain stable output when power supply is stable, wiring is standardized, and transmission distance is reasonable, but voltage signals are relatively sensitive to line voltage drop and external interference. If the transmission distance is long, 4-20mA current signals generally offer greater advantages; if multipoint data acquisition is required, 485 or other digital communication solutions should be prioritized.
The actual transmission distance of RS485 is affected by baud rate, cable quality, topology, and the electromagnetic environment. Reliable transmission distances commonly reach several hundred meters in engineering applications and can be extended further under low baud rates, standardized wiring, and good anti-interference conditions. The greater the distance, the more attention should be paid to isolation, shielding, terminal matching, and surge protection.
IV. Measurement Recommendations for Viscous Media and Wireless Applications
Are piezoelectric level sensors suitable for viscous liquids?
Whether viscous liquids are suitable for piezoelectric or other level measurement principles depends on whether the medium adheres, foams, crystallizes, and whether agitation is present inside the vessel. High-viscosity media can easily form buildup on the probe surface. If the measurement principle is sensitive to contact conditions or vibration characteristics, readings may be affected.
For grease, adhesives, resins, slurries, syrups, or liquids containing suspended particles, it is recommended to conduct medium testing first, focusing on zero-point changes after buildup, repeatability, and cleaning recovery capability. If necessary, diaphragm structures, non-contact measurement methods, or installation solutions with flushing conditions can be selected.
If continuous agitation, a foam layer, or liquid surface fluctuations are present inside the vessel, the sensor installation location should avoid the feed inlet, return inlet, and areas near agitator blades. For operating conditions with noticeable fluctuations, a suitable filtering time can be set through the control system to prevent transient disturbances from frequently triggering alarms or start-stop actions.
Proper measuring range configuration is also important. For example, if the actual level variation range is 0 to 3 meters, an excessively large range should not be selected arbitrarily, as this may sacrifice effective resolution. Selection should also not be made too close to the upper limit; calculations should take liquid density, hydrostatic pressure variation, and vessel allowance into account.
Are wireless level sensors safe for use in mines?
The safety of using wireless level sensors in mines first depends on compliance with the explosion-proof and communication management requirements of the mining project. A mine environment is not an ordinary indoor wireless environment; factors such as combustible gases, metal structure obstruction, tunnel reflections, power supply limitations, and signal coverage blind spots must be considered.
In areas with explosion-proof requirements, sensors, wireless terminals, power supplies, batteries, and supporting installation accessories must all be evaluated as a complete system. It is not sufficient to confirm that the sensor itself has a certain capability while overlooking potential site risks caused by charging equipment, wiring methods, or gateway deployment.
Wireless solutions are suitable for difficult wiring conditions, dispersed equipment, or temporary monitoring requirements, but critical interlock control should not rely entirely on unverified wireless links. For important control points such as drainage pump protection and shutdown due to excessive level, a wired primary signal combined with wireless data-assisted monitoring can be adopted to improve system availability.
Before project implementation, on-site signal testing should be completed to record communication quality, packet loss, and power endurance at different locations. For projects requiring continuous operation, it is recommended to establish communication interruption alarms, data caching, and manual inspection mechanisms to prevent equipment from remaining offline undetected for extended periods.
V. How to Rationally Compare Domestic and Imported Level Sensors
Imported level sensors are more expensive, usually due to factors such as brand investment, certification systems, global supply chains, channel costs, production scale, and specific technical expertise. However, a higher price does not automatically mean a product is more suitable for the site, nor are domestic products limited to low-requirement operating conditions. What truly matters is whether parameters, materials, delivery time, service, and system compatibility meet project requirements.
For conventional water treatment, equipment integration, general storage tanks, and automated production lines, domestic level sensors with stable performance, suitable measuring ranges, and compatible signals can generally meet usage requirements, while offering flexible delivery cycles, efficient communication, and rapid response for non-standard customization. For projects involving high temperatures, high pressures, extremely strong corrosion, or special certifications, comparisons should be made carefully according to technical specifications.
Procurement evaluation should not compare only the unit quotation; total lifecycle cost should also be calculated. This includes installation modification costs, spare part lead times, calibration and maintenance, fault response, downtime losses, and the difficulty of subsequent capacity expansion. A solution with a lower initial purchase price but frequent failures may incur higher long-term costs than a stable and reliable configuration.
During the inquiry stage, it is recommended to provide suppliers with complete operating condition information: medium name, density, maximum temperature, maximum pressure, measurement height, installation interface, supply voltage, output method, accuracy requirements, and application area. The more complete the information, the more closely the level sensor solution provided by the manufacturer will match actual operating requirements.
When level sensors are required for storage tanks, pools, acid and alkali containers, oil tanks, or automated equipment, organize the on-site medium, measuring range, installation dimensions, and control system interface parameters, and contact Xi'an Shenghongchuang Instrumentation Co., Ltd. for targeted product selection, non-standard customization, and technical support solutions.
- Piezoelectric Level Sensor
- PTFE Level Sensor
- Domestic Level Sensors
- Wireless Level Sensor
- 1-5V Level Sensor
- Imported Level Sensor
- HART Protocol Level Sensor
- RS232 Level Sensor
- Sealed Level Sensor
- Linear Level Sensor
- Digital Display Instrument
- Which industries are suitable for level sensors with good linearity?
- Will a sealed level sensor leak when used in coal mines?
- Can an RS232 level sensor be connected to a PLC?
- Which is better: a HART protocol level sensor or an RS-485 level sensor?
- Are wireless level sensors safe for use in mines?
- Can PTFE level sensors be installed in strong acids?
- Are piezoelectric level sensors suitable for viscous liquids?
Related Recommendations
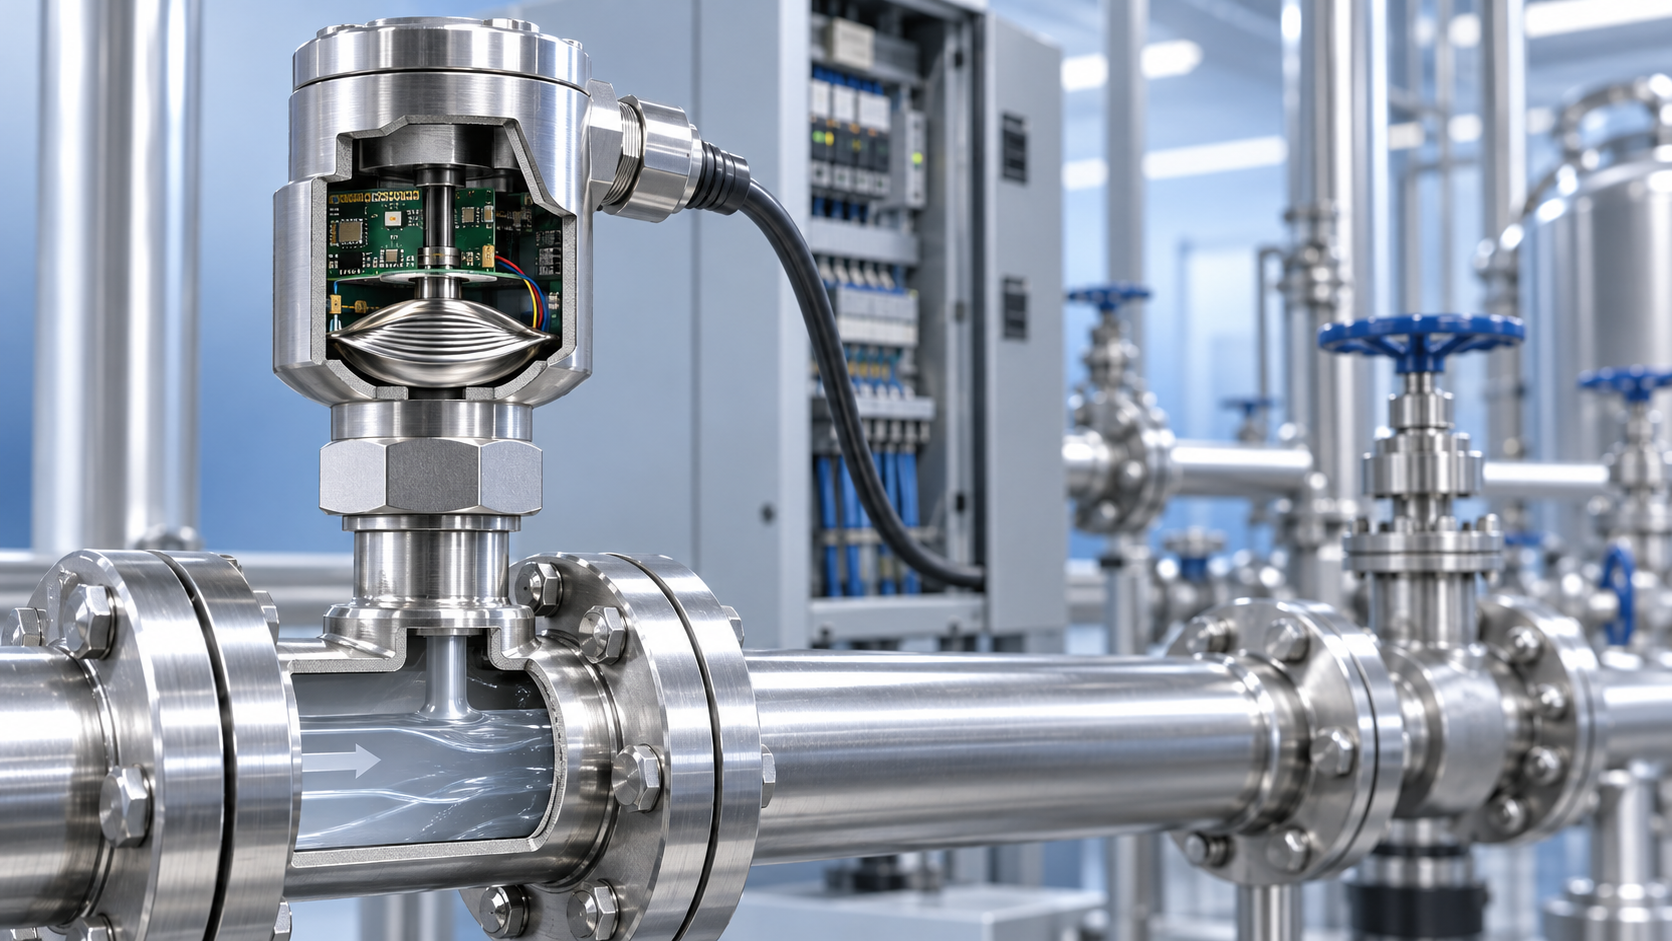
 How does a pressure sensor convert changes in applied force into usable electrical signals?
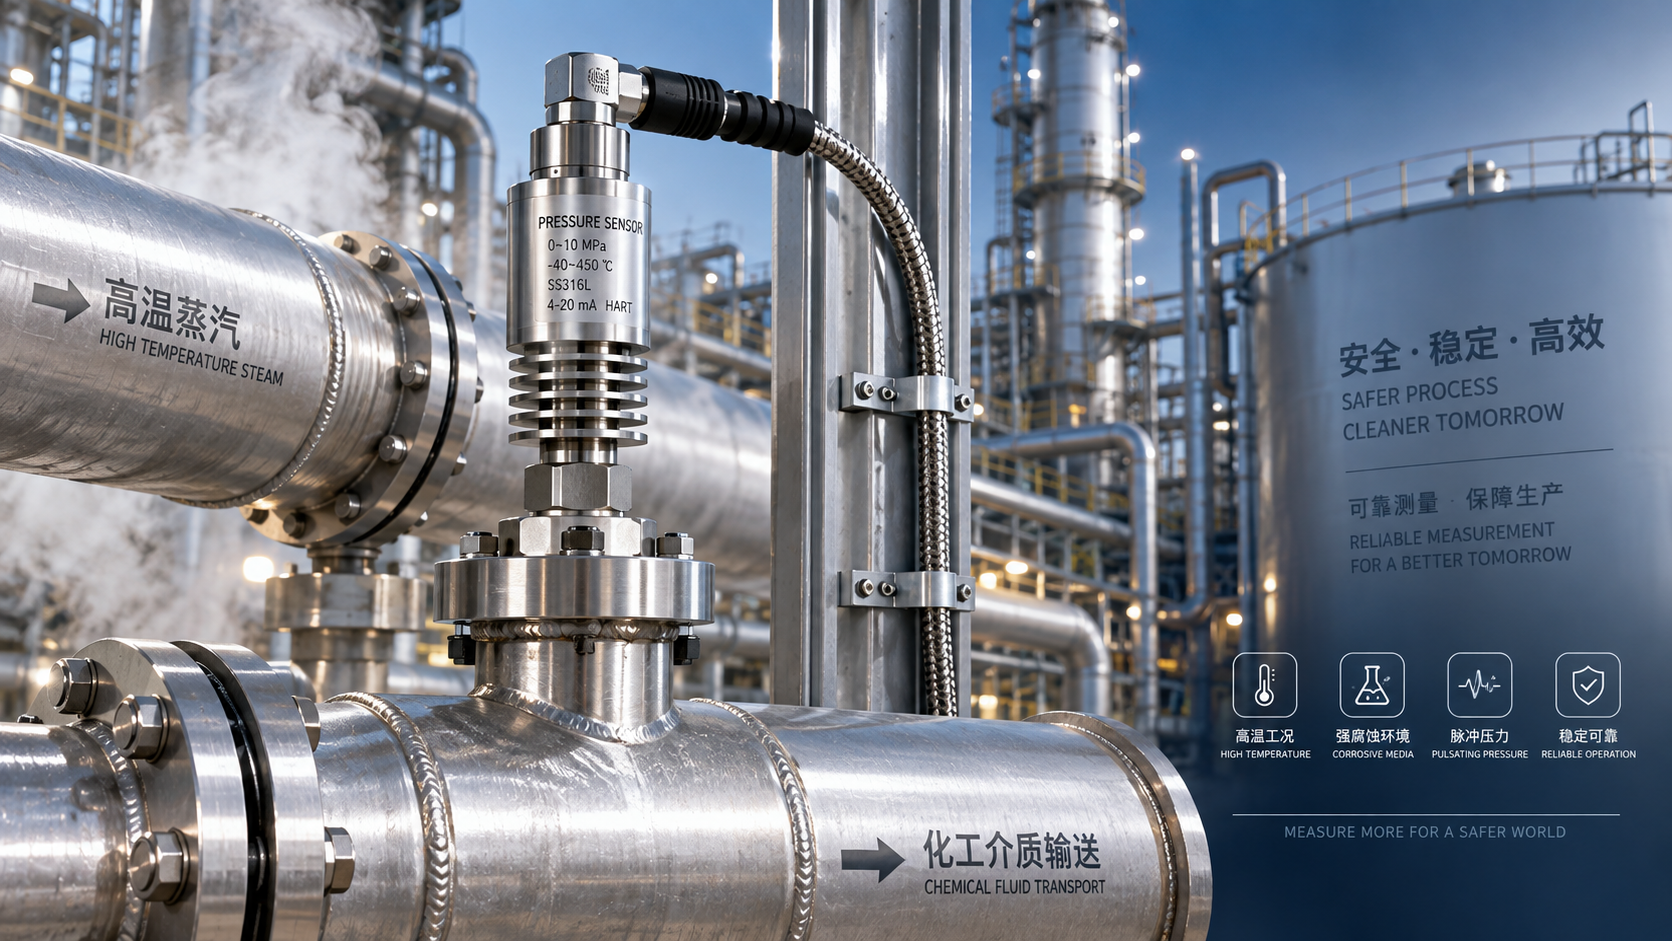
 Which parameters should be considered when selecting pressure sensors for high-temperature, corrosive, and pulsating operating conditions?
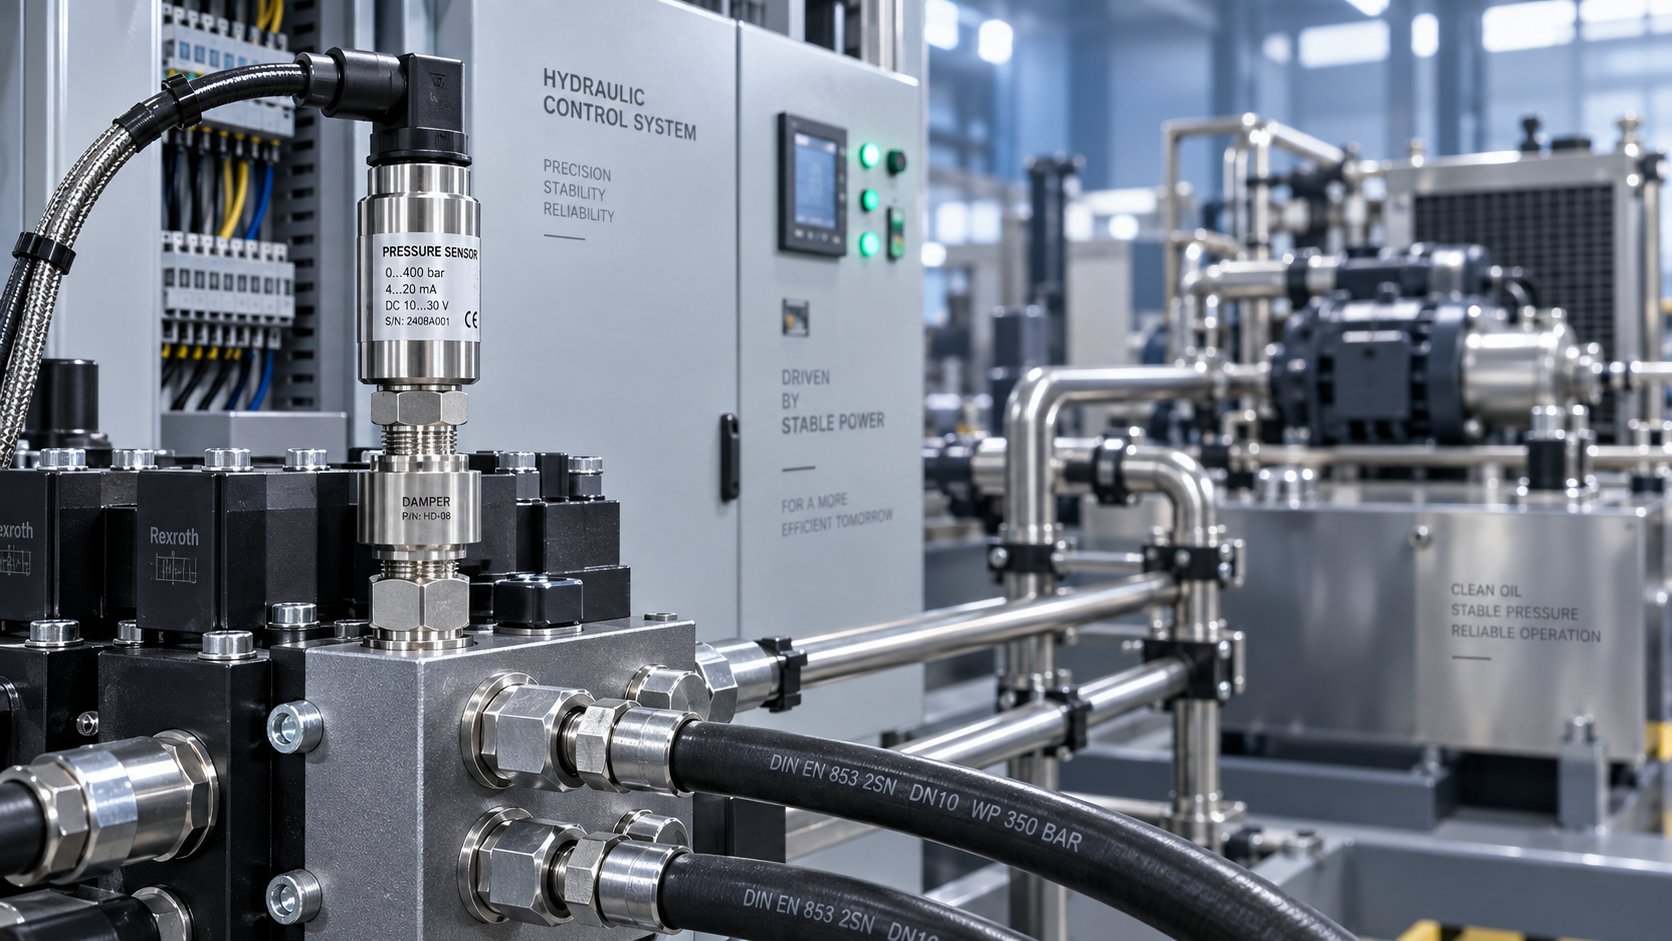
 Hydraulic equipment pressure fluctuates frequently. How can sensors be configured to improve control stability?
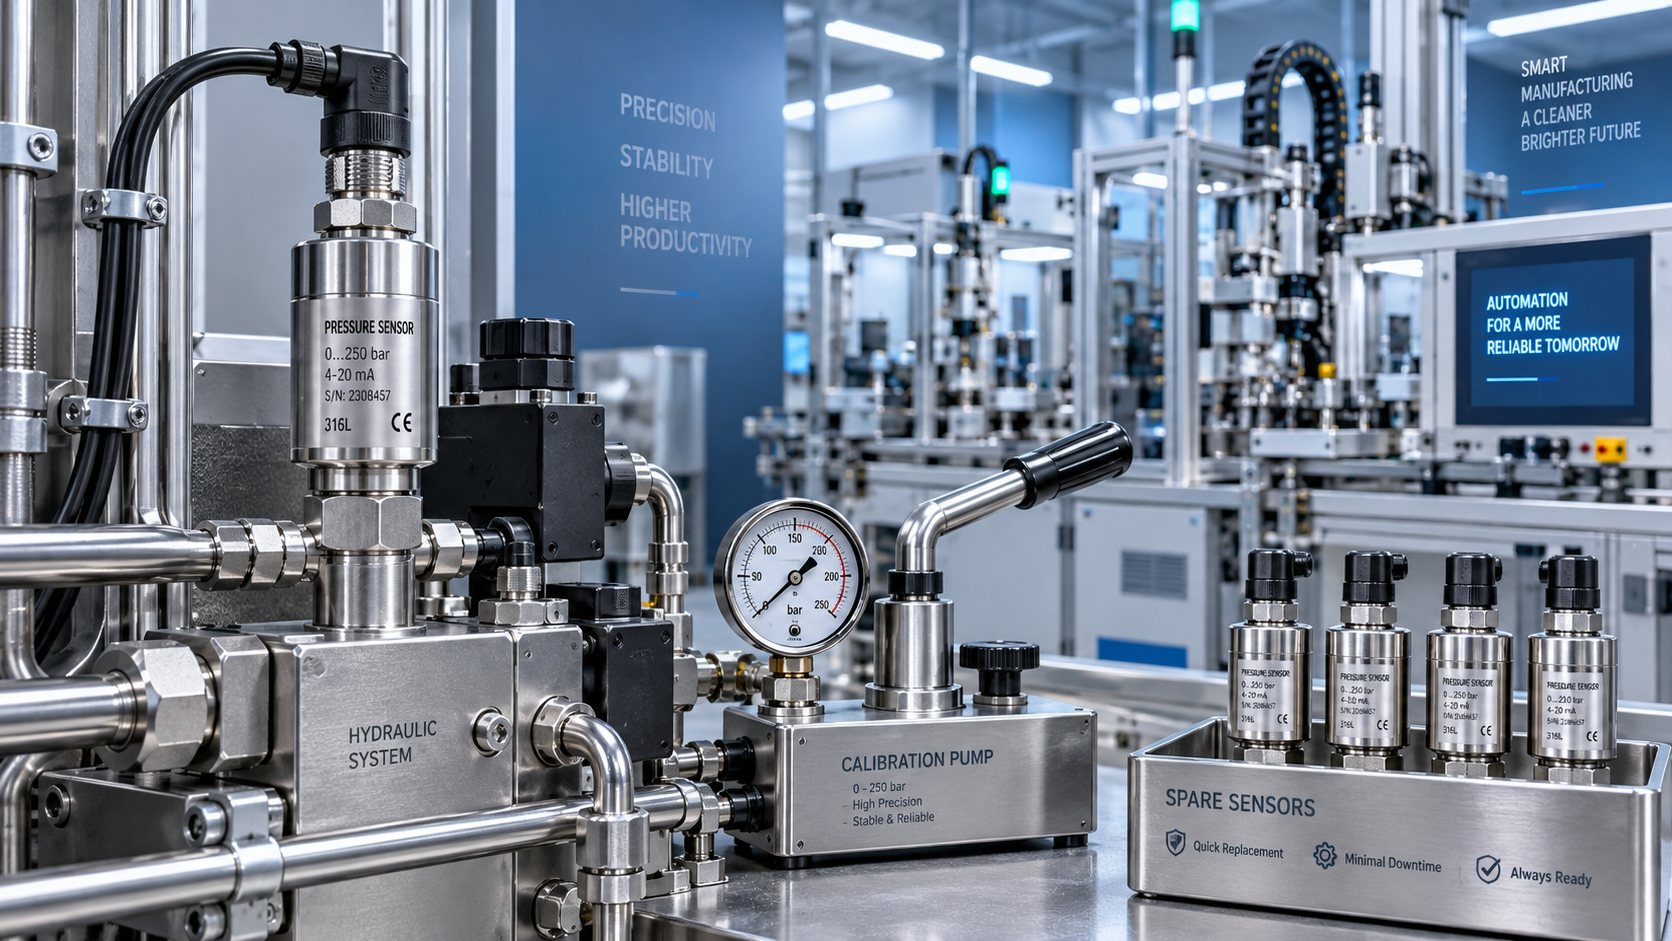
 When purchasing pressure sensors, how can you evaluate service life and total maintenance costs beyond the unit price?