


News Center
—— NEWS CENTER ——
Xi'an Shenghongchuang Instrument Co., Ltd.
Contact: Mr. Zhang
Mobile: 15529283736
Email: shc-sensor@qq.com
Address: Fortune Building, Sanqiao Street, Xixian New Area, Xi'an, Shaanxi Province
How to Audit a Pressure Transmitter Factory for Long-Term Export Cooperation
Before entering into long-term export cooperation, a pressure transmitter factory audit should not rely solely on sample prices, promotional materials, or sales representatives’ commitments. Export orders typically involve batch delivery, cross-border transportation, local certification, after-sales response, and long-term spare parts supply. A loss of control in any one of these areas may escalate into risks of production shutdowns, claims, or customer loss.
For business decision-makers, the core purpose of a factory audit is not to determine whether a manufacturer “appears large in scale,” but to confirm whether it has the capabilities for stable manufacturing, accurate calibration, complete traceability, timely delivery, and ongoing service. Particularly for pressure transmitters used in chemical processing, energy, machinery and equipment, automated production lines, and similar applications, reliability is often more important than the cost of a single purchase.
Taking the dual-base operating model of Xi'an Shenghongchuang Instrument Co., Ltd. and its production base, Shaanxi Qinkong Sensor Technology Co., Ltd., as an example, brand operations, sales and technical services, and the standardized manufacturing base undertake different functions. Buyers should form an actionable supplier evaluation conclusion through four stages: document review, on-site visits, sample verification, and small-batch trial orders.
I. First Verify the Basic Qualifications Required for Export Cooperation
Confirm the Legal Entity, Production Site, and Product Liability Boundaries
The first step of a factory audit is to verify the business license, production address, brand authorization relationship, trademark use rights, and actual manufacturing entity. The supplier, invoicing entity, manufacturer, and after-sales responsible party stated in the export contract should be as clearly aligned as possible, avoiding situations in which a brand company takes the order, a third-party factory manufactures the products, and the liable entity is difficult to trace.
For sensor companies using a dual-base operating model, buyers should confirm on site the division of responsibilities between the office center and the manufacturing facility. For example, the sales center may be responsible for technical coordination and export documentation, while the production base handles machining, assembly, calibration, testing, and final inspection. Whether the information systems of both sides can correspond to the same product batch should also be included in the audit.
Pressure transmitters are metering and industrial measurement and control products. In addition to the company's basic licenses and certificates, attention should also be given to applicable product standards, testing capabilities, and target-market access requirements. Requirements for CE, RoHS, EMC, explosion protection, classification society approvals, or specific industry documents vary by country and project. Domestic documentation for standard models cannot simply replace export compliance documents.
It is recommended to request a list of export products from the past 12 months, major destination markets, typical industry applications, and samples of relevant documents. The materials do not need to involve customer confidentiality, but they should demonstrate whether the manufacturer truly understands the practical requirements for English nameplates, technical specifications, packing lists, certificates of origin, and export packaging markings.
Key Documents to Review During Qualification Verification
Document review should not stop at whether certificates are available. It should also verify whether the document name, model, validity period, issuing authority, and actual product configuration are consistent. For example, documentation for an ordinary pressure transmitter cannot directly cover an explosion-proof model, and test documents for a 4-20mA output model do not automatically apply to an RS485 communication version.
Buyers may randomly select three recently shipped production batches and require the manufacturer to retrieve the corresponding orders, production routing sheets, calibration data, and packaging records. If the model, range, accuracy class, supply voltage, and serial number can be matched in a closed traceability loop across these documents, its basic management capability is relatively reliable.
For long-term cooperation projects, it is advisable to include document update obligations in the purchasing agreement. Changes in certification status, replacement of key components, adjustments to the production address, production discontinuation alerts, and specification changes should all be notified to the buyer in writing before shipment to avoid undisclosed changes to products with the same name.
II. Enter the Workshop to Assess Actual Capacity and Process Control
Capacity Depends Not Only on Plant Area but Also on Production Scheduling Logic
Pressure transmitter lead times are jointly affected by housing machining, sensor cores, electronic circuits, connection materials, potting processes, calibration stations, and aging tests. Simply seeing an ample inventory of samples does not prove that a manufacturer can consistently fulfill export orders of 500 units, 1,000 units, or even larger quantities.
During the factory audit, ask about monthly capacity, normal lead times, peak-season lead times, and mechanisms for urgent inserted orders for both standard and non-standard models. For common diffused silicon pressure transmitters, the production pace of standard-configuration orders is usually directly related to inventory availability of core sensor elements. For high-temperature, high-pressure, sanitary, flanged level, or special-thread products, the procurement lead times for key components should be confirmed separately.
On site, observe whether the raw material area, assembly area, calibration area, and finished goods area are clearly separated; whether semi-finished products have process identification; and whether items pending inspection are isolated from qualified products. If products with different ranges, output signals, or customer labels are mixed on the same workbench, the probability of incorrect shipments in export batches will increase significantly.
Shaanxi Qinkong Sensor Technology Co., Ltd. has a standardized intelligent manufacturing facility. However, buyers should still rely on on-site records and focus on confirming equipment utilization, staffing at workstations, and the number of work-in-process orders. Actual capacity must withstand cross-verification from three dimensions: order scheduling, inventory of key materials, and testing bottlenecks.
Recommended Production and Delivery Metrics for Spot Checks
When sourcing pressure transmitters for international trade, a common mistake is treating a “promised delivery time” as “verifiable capacity.” For initial cooperation, it is recommended to use a small-batch trial order of 100 to 300 units, record the complete cycle from technical confirmation, drawing confirmation, and production scheduling to factory shipment, and then determine the purchasing volume for an annual framework order.
For orders requiring customized connections, special ranges, or customer English labels, the sample freeze date should be clearly confirmed. Once the sample is approved, the range, thread, diaphragm material, output method, cable length, and packaging labels should all be included in change control to avoid repeated modifications during mass production that lead to delivery delays.
Export packaging should also be physically inspected during the factory audit stage. Each unit should preferably have shockproof inner padding, an individual identification label, and necessary moisture-proof measures. Outer cartons should indicate the model, quantity, gross and net weight, and carton number. For long-distance sea transportation, the manufacturer may be required to provide drop-test records or simulated transportation packaging validation records.
III. Make Calibration and Testing Capability the Core of the Factory Audit
Observe the Calibration Process Rather Than Only Inspecting Test Equipment
The core value of a pressure transmitter lies in measurement accuracy. During a factory audit, attention should be given to whether the manufacturer can effectively control zero point, full scale, linearity, repeatability, hysteresis, and output stability, rather than merely looking at how many verification or calibration certificates are displayed on the wall.
It is recommended to randomly select finished products on site and observe the complete process, from connection to the pressure source, power supply, and output acquisition equipment, through point-by-point pressurization, return-stroke testing, data recording, and conformity assessment. For 4-20mA products, verify whether the zero point is close to 4mA and whether full scale is close to 20mA, and check whether process data are automatically saved or manually reviewed.
Different accuracy classes correspond to different application risks. For general industrial control, a 0.5%FS class may be appropriate, while demanding process control or laboratory equipment may require 0.25%FS or even higher accuracy. Buyers must clearly specify in the contract whether the accuracy basis is full scale FS, reading RD, or overall accuracy; otherwise, the parties may have different interpretations of “meeting the requirement.”
For export orders with a wide range span, one sample report cannot cover all specifications. There are differences in calibration equipment, pressure media, and safety protection requirements for ranges of -0.1MPa to 0MPa, 0MPa to 1MPa, 0MPa to 10MPa, and higher pressure ranges, so actual testing capabilities should be confirmed separately.
Key Calibration and Performance Verification Items
The calibration status and validity period of reference instruments should be checked, and their ranges should be confirmed to cover the products under test. Under normal circumstances, the accuracy of the reference instrument should be better than that of the product being tested to ensure that calibration results are meaningful. If a manufacturer can only test low-pressure models but accepts high-pressure orders, subsequent quality risks will become concentrated.
It is recommended to require traceable factory inspection records for each product or each batch, including at least the model, range, output signal, power supply, accuracy class, inspection date, inspector, and serial number. For critical projects, five-point or six-point calibration data may be required instead of merely issuing a general conclusion of “inspection passed.”
When a pressure transmitter experiences accuracy drift after six months of use, after-sales assessment requires support from original data. Complete factory calibration records can help distinguish between initial product deviation, on-site overpressure, media corrosion, temperature effects, installation stress, or electromagnetic interference, avoiding prolonged uncertainty regarding after-sales responsibility.
For high-temperature, high-humidity, high-vibration, or chemically corrosive environments, the factory audit should also inquire about temperature compensation, aging tests, sealing tests, and media compatibility validation methods. The product's rated operating temperature, storage temperature, and protection rating must match actual application conditions and cannot be selected solely based on room-temperature laboratory data.
IV. Evaluate Quality Traceability, Warranty, and After-Sales Response
Long-Term Cooperation Requires a Batch Traceability Mechanism
Export orders span multiple stages including transportation, storage, installation, and end use. When a product issue occurs, the most important task is to quickly identify the scope of impact. The manufacturer should be able to trace, through a serial number or batch number, the production date, core materials, assembly personnel, calibration records, inspection results, and shipping carton number.
During a factory audit, a simulated question can be raised: if a customer reports an abnormal zero point on a 0-1.6MPa product with 4-20mA output, can the manufacturer identify the production batch and factory data within 24 hours? Can it determine whether other products in the same batch have potential risks? This is more valuable for assessment than simply asking whether after-sales service is available.
A warranty period of 12 to 18 months is generally common for exported pressure transmitters, but the specific duration should be determined in conjunction with the product type, operating conditions, installation responsibilities, and transportation terms. For customized products, it is advisable to clearly state whether the warranty begins on the shipment date, arrival-at-port date, or end-user acceptance date to avoid differences in interpretation.
When technical parameters fail to meet requirements, the contract should specify the reinspection method, acceptance criteria, return and replacement procedures, freight responsibility, and resolution time limits. For batch quality issues, sampling inspection ratios, allowable defect rates, and mechanisms for reinspection of the entire batch may be established, preventing buyers from having to communicate unit by unit after receipt and affecting project progress.
Do Not Rely Only on Manufacturer Rankings; Assess Ongoing Service Capability
Pressure transmitter manufacturer rankings can serve as an initial source of information, but rankings are usually influenced by brand exposure, sales volume, platform data, and regional markets. They cannot replace a factory audit for a specific model. Suppliers genuinely suitable for long-term export cooperation should be able to withstand verification in technical response, batch consistency, documentation capability, and after-sales closed-loop management.
Whether domestically manufactured pressure transmitters can replace imported products depends on application conditions rather than origin labels. For conventional industrial measurement, equipment integration, and automation upgrade projects, domestically manufactured products that have undergone standardized selection, sample verification, and batch consistency control usually offer good cost performance. For extreme operating conditions or specified-brand projects, each item should be evaluated based on certification, service-life data, and end-user requirements.
Selecting only low-priced products may result in higher maintenance costs later. One shutdown, one cross-border repair return, or one on-site recalibration often exceeds the purchase price savings of a single product. Purchasing decisions should compare the initial purchase price, expected failure rate, spare parts supply, warranty terms, and technical response speed at the same time.
It is recommended to stipulate technical response time limits in annual cooperation agreements. For example, general technical inquiries should be answered within 1 working day, preliminary analysis of quality abnormalities should be submitted within 24 hours, and a resolution plan for major batch issues should be provided within 72 hours. For overseas projects, the specific procedures for English technical support, remote commissioning, and supplementary spare parts shipments should also be confirmed in advance.
V. Implement Factory Audit Conclusions Through Trial Orders and Contracts
Progress from Small-Batch Verification to Long-Term Cooperation
After a factory audit is passed, it is not advisable to immediately concentrate the entire purchasing volume with a single supplier. First, select representative ranges, connections, outputs, and environmental requirements for a small-batch trial order to verify whether product accuracy, packaging integrity, actual delivery time, English documentation, and after-sales response are consistent with the factory audit conclusions.
Trial-order acceptance should cover incoming inspection, power-on testing, pressure comparison, on-site installation, and operational observation. For critical equipment, phased retest plans at 30, 90, and 180 days may be established to monitor zero drift, output stability, sealing performance, and suitability for operating conditions, rather than merely confirming that the appearance is undamaged on the day of receipt.
The contract should clearly specify the model code, range, accuracy class, process connection, wetted material, output signal, protection rating, packaging method, acceptance criteria, and warranty responsibility. Any parameter considered important by the buyer should be included in the technical annex rather than relying solely on chat records or brief descriptions in quotations.
For pressure transmitter procurement projects planned for long-term export, technical, quality, purchasing, and logistics personnel may jointly complete supplier scoring. Qualification compliance, manufacturing capability, testing capability, delivery performance, and after-sales capability should be separately scored quantitatively to form the basis for annual reviews, shifting supplier management from experience-based judgment to sustainable quality control.
To assess the conditions for long-term pressure transmitter export cooperation, target market, application medium, range, accuracy, connection, signal, and estimated annual purchase volume may be submitted to Xi'an Shenghongchuang Instrument Co., Ltd. Product documentation verification, manufacturing base inspection, and sample trial-order validation can then be arranged to confirm technical and quality standards before advancing stable export cooperation.
Related Recommendations
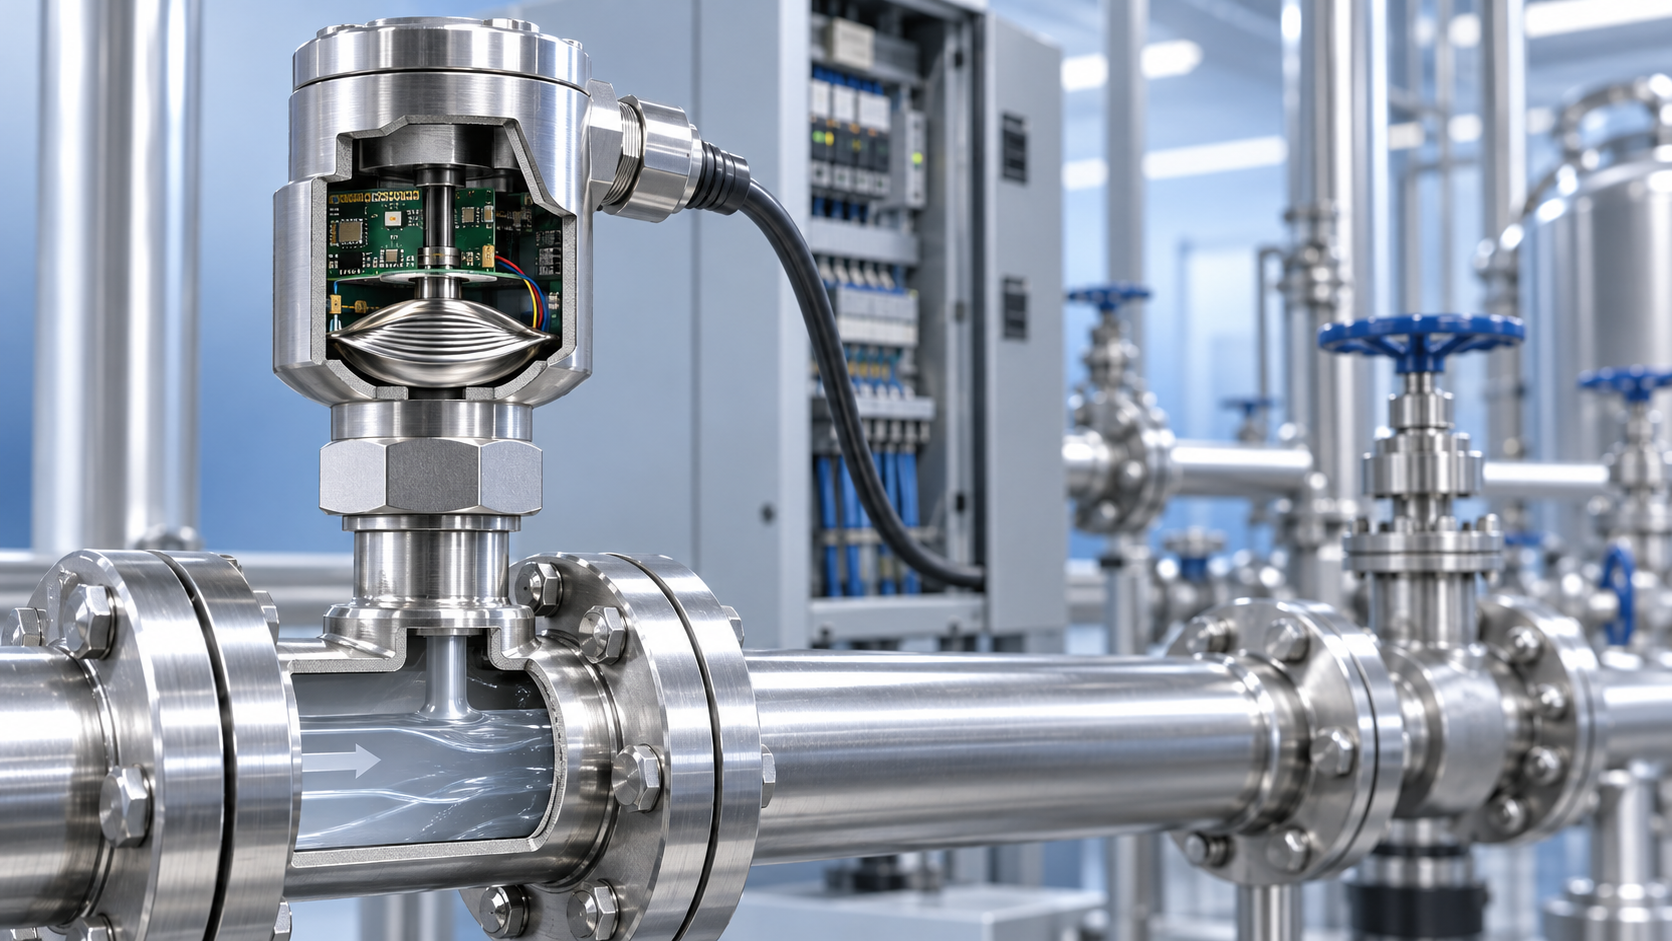
 How does a pressure sensor convert changes in applied force into usable electrical signals?
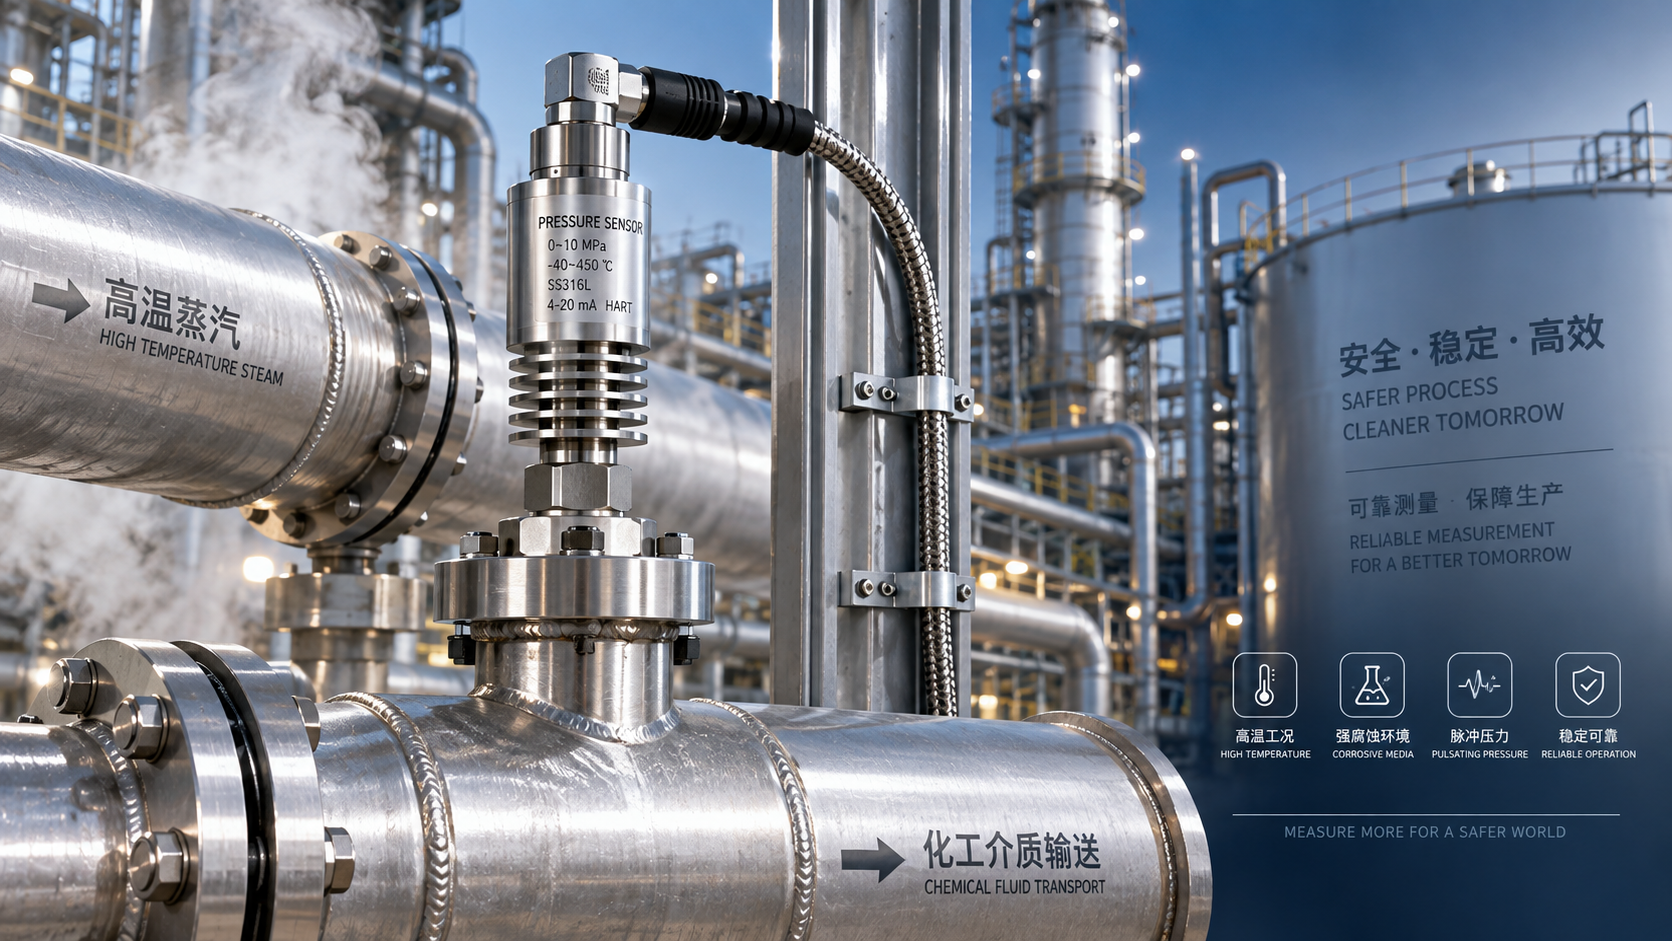
 Which parameters should be considered when selecting pressure sensors for high-temperature, corrosive, and pulsating operating conditions?
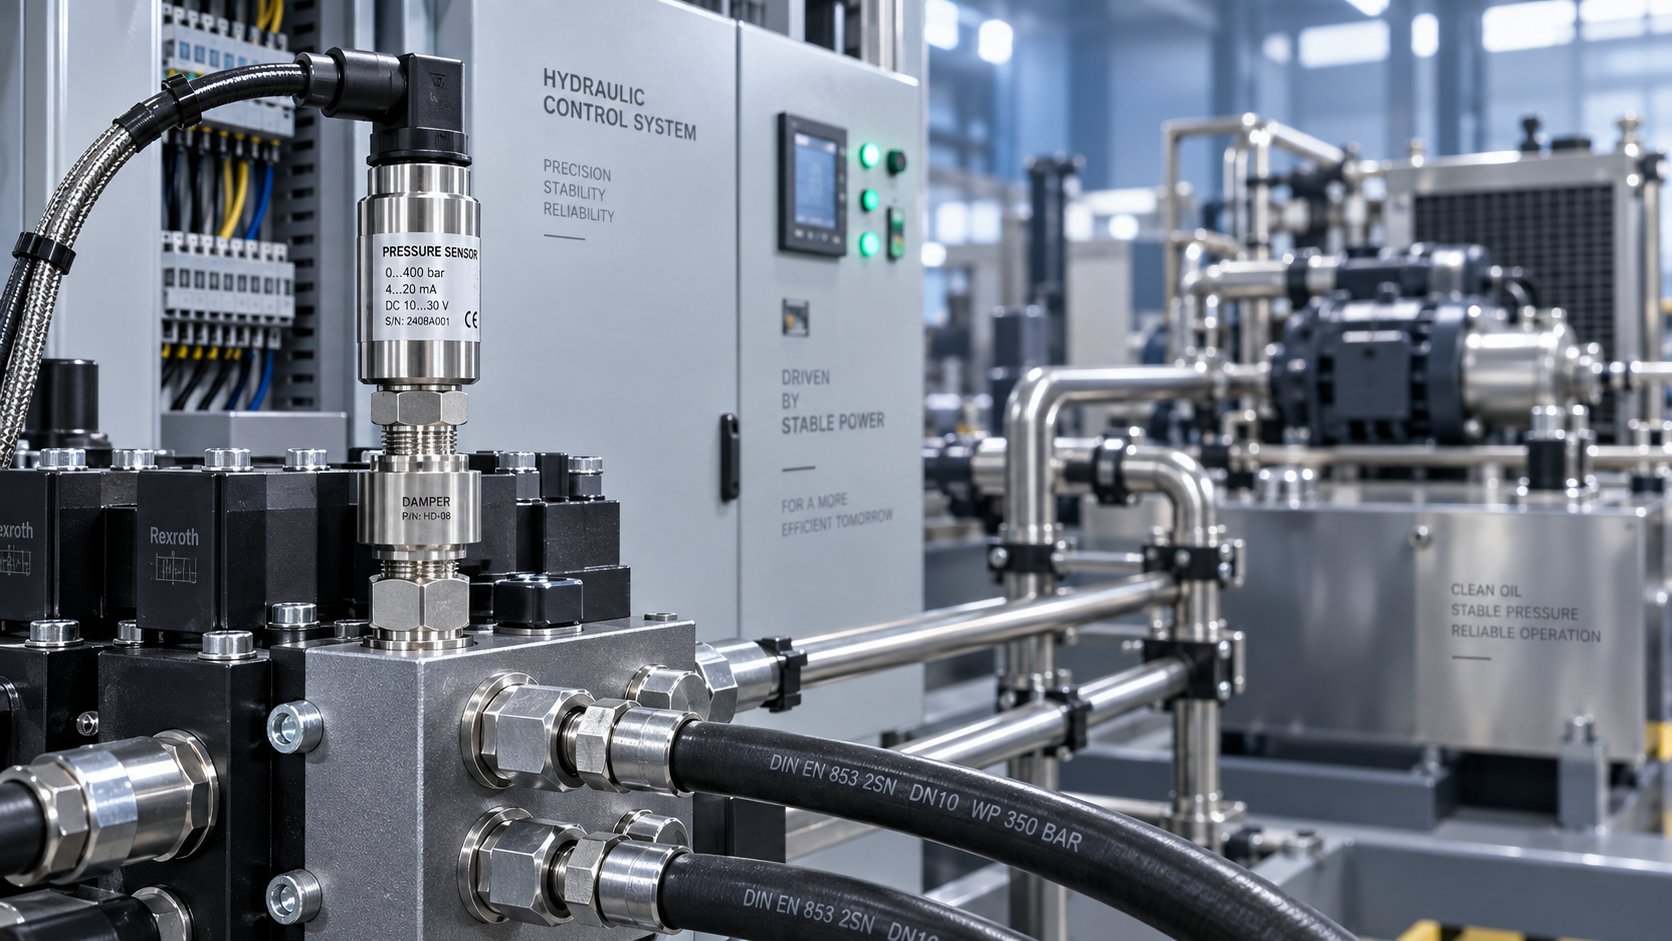
 Hydraulic equipment pressure fluctuates frequently. How can sensors be configured to improve control stability?
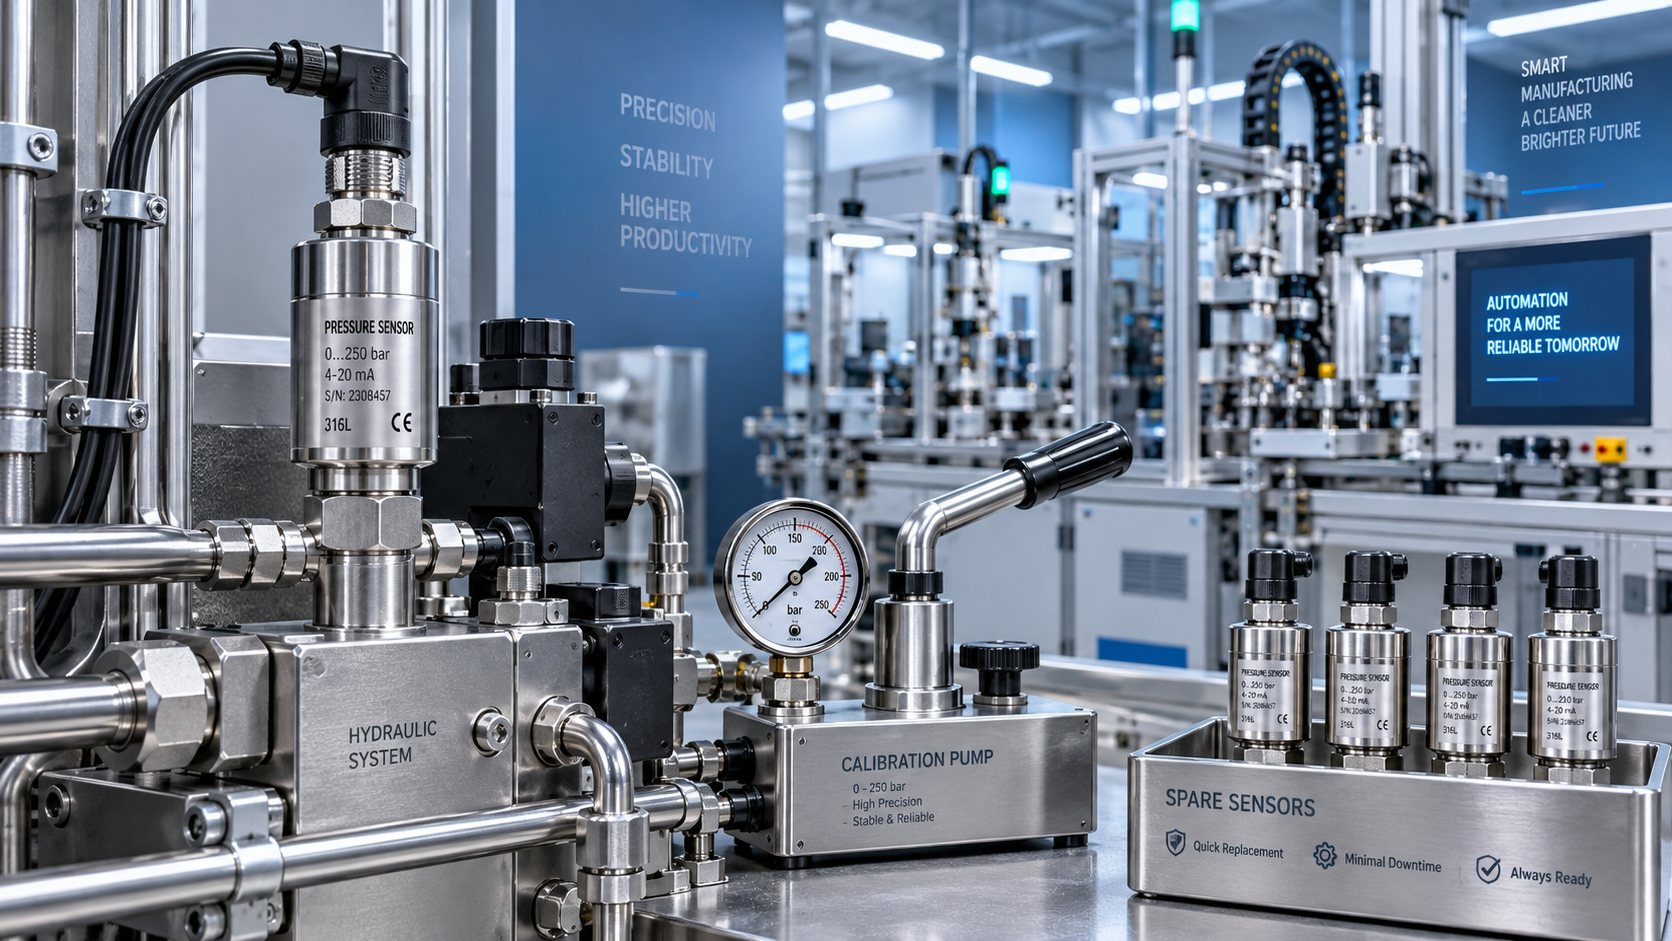
 When purchasing pressure sensors, how can you evaluate service life and total maintenance costs beyond the unit price?